China Best Supply Chain Optimization Supplier & Exporter

Guangdong Ebil Metal Products Co., Ltd. — Next-Generation Smart Warehouse Storage Racking & Intelligent Automation Systems Engineered for High-Density Global Logistics

Automated Storage & Core Systems

High-Density Warehouse Optimization Hardware

Explore our flagship automated radio pallet shuttles, heavy-duty self-supporting steel racking, and dynamic mezzanine floor systems built for global enterprises.

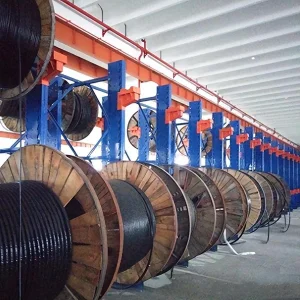
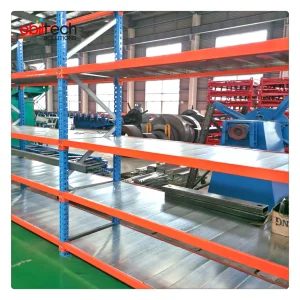
Warehouse Store Wires and Cables Racks- Wire Spool Racking
View Specifications
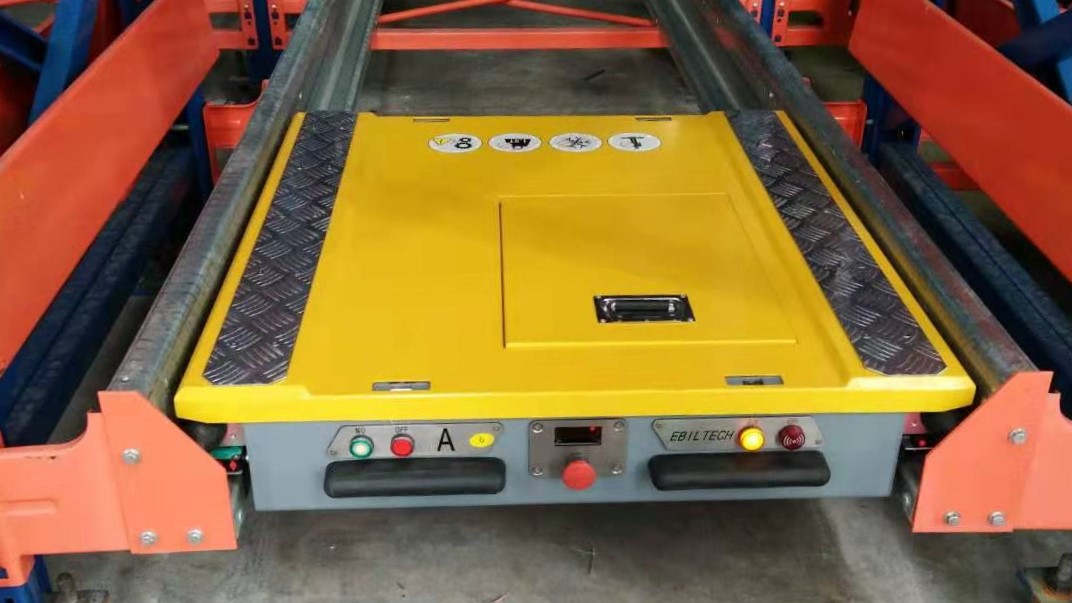
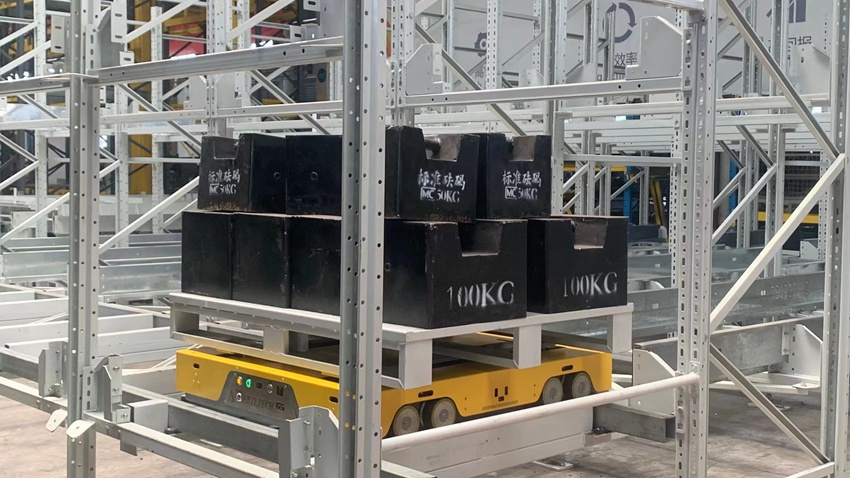
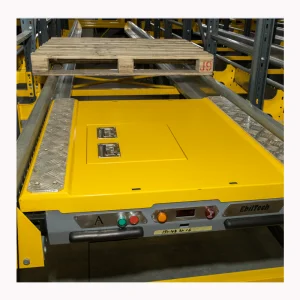
EBILTECH 500-2000kg Load Automated Access Equipment Radio Pallet Shuttle Car
EBILTECH 500-2000kg Load Radio Pallet Shuttle Car (CE Certified)
View Specifications
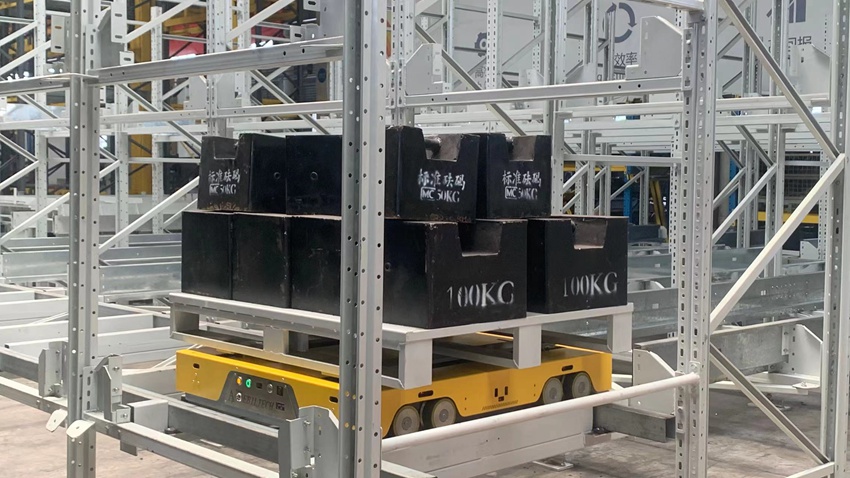
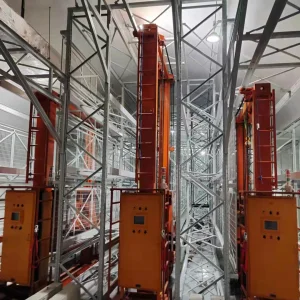
EBILTECH Pallet Racking Robot Shuttle System Warehouse Storage Carts
EBILTECH Pallet Racking Robot Shuttle System Warehouse Carts
View Specifications
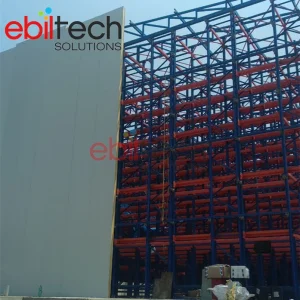
Steel Clad Self-Supporting Heavy Duty Racking System
Professional Steel Clad Self-Supporting Multi-Layer Racking System
View Specifications
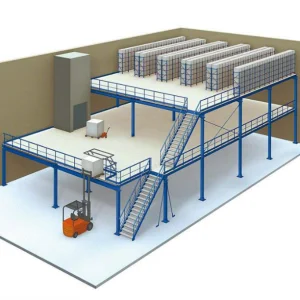
Steel Mezzanine Floor Racking Long Span Shelves
Steel Workshop Platform Warehouse Mezzanine Floor Racking
View Specifications
Wholesale Mezzanine Warehouse Storage Racks
Wholesale Multi-Level Warehouse Storage Mezzanine Floor Racks
View Specifications
Automated Mobile Racking System Shelving
Material Rack Automated Storage Electric Mobile Racking System
View Specifications
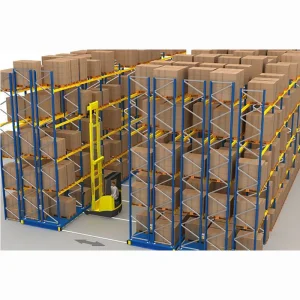
Automated Warehouse Storage Radio Pallet Shuttle System
Automated Storage Equipment Radio Pallet Shuttle Bins System
View Specifications
Industry Whitepaper & Strategic Insights

Navigating Modern Supply Chain Optimization & Spatial Architecture

An in-depth analysis of global procurement shifting toward high-density automated racking, structural load management, and smart fulfillment hubs.

1. Macro Trends Reshaping Supply Chain Optimization (2025–2030)

Global supply chains are enduring unprecedented shifts. Driven by skyrocketing commercial real estate costs, labor shortages, and rising e-commerce customer expectations, logistics managers can no longer rely on static floor storage or single-deep selective racking. Modern supply chain optimization requires transitioning from horizontal expansion to vertical volume utilization.

  • Maximum Footprint Yield: Automated Shuttle and AS/RS systems increase structural cubic storage density by up to 85% compared to conventional aisle configurations.
  • Operational Cost Mitigation: High-density automated racking drastically cuts forklift travel distance, energy consumption, and product damage caused by manual handling.
  • Nearshoring & Multi-Tier Hubs: Regional distribution centers demand scalable, modular structural racking systems capable of handling multi-SKU profiles with rapid cycle times.

2. Structural Engineering & Load Optimization Matrices

Deploying heavy-duty warehouse infrastructure demands rigorous structural engineering. Factor metrics such as deflection ratios, seismic zone calculations (PGA factors), post-yield steel stress analysis, and dynamic load coefficients dictate long-term system integrity.

At Guangdong Ebil Metal Products Co., Ltd., structural design leverages premium cold-rolled Q235B and Q355B high-tensile steel profiles. Automated finite element analysis (FEA) ensures every upright frame, beam loading capacity, and baseplate distribution meets strict international safety margins, minimizing steel fatigue under dynamic forklift impact.

Manufacturing Authority & E-E-A-T Excellence

Guangdong Ebil Metal Products Co., Ltd.

A trusted global leader in engineering, manufacturing, and exporting enterprise-grade industrial warehouse racking and automated logistics systems.

Guangdong Ebil Metal Products Co., Ltd. is a professional manufacturer specializing in industrial storage systems and warehouse racking solutions. We design, manufacture, and supply high-quality shelving and storage equipment for warehouses, distribution centers, factories, retail stores, logistics companies, and commercial facilities worldwide.

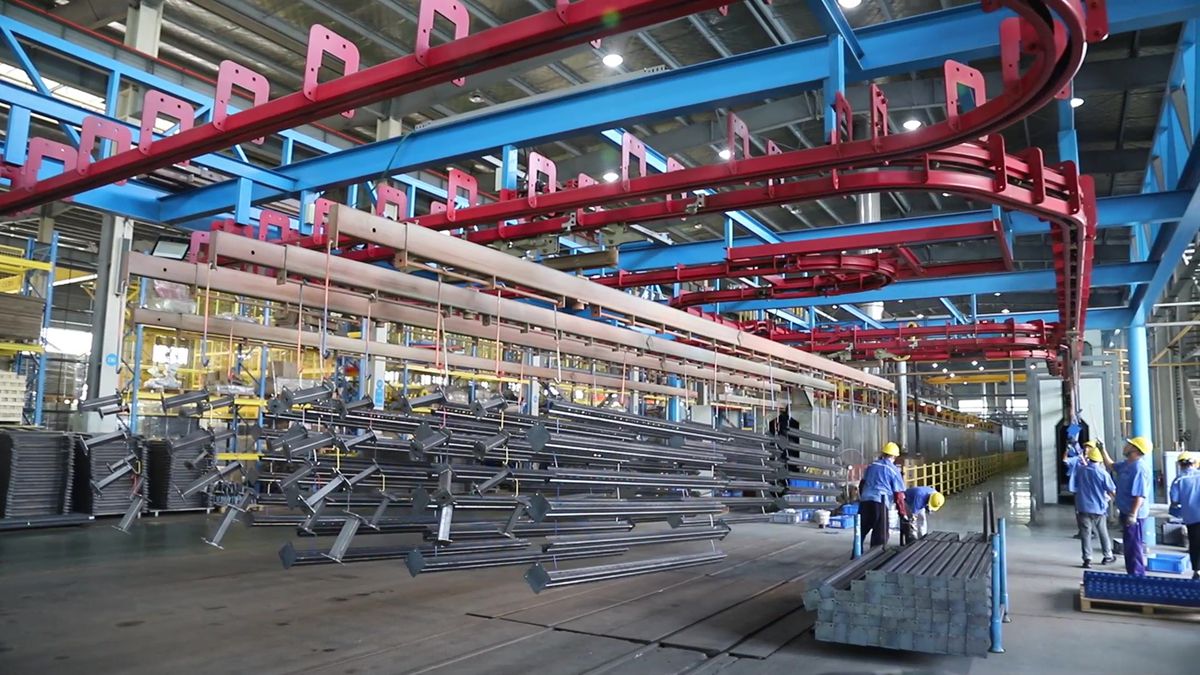
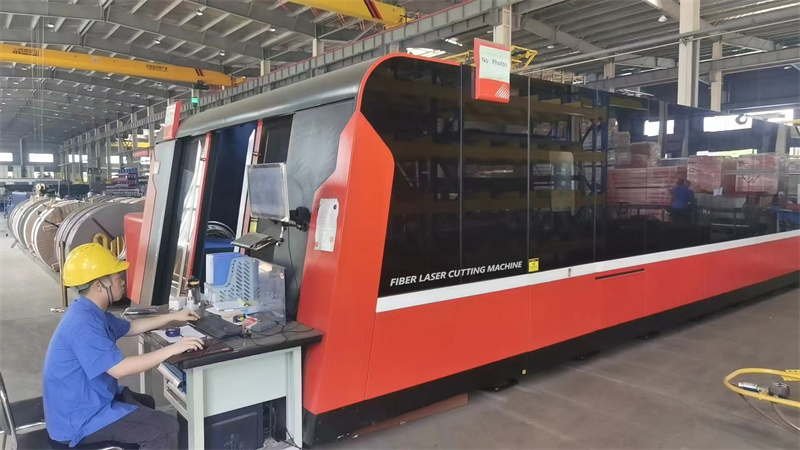
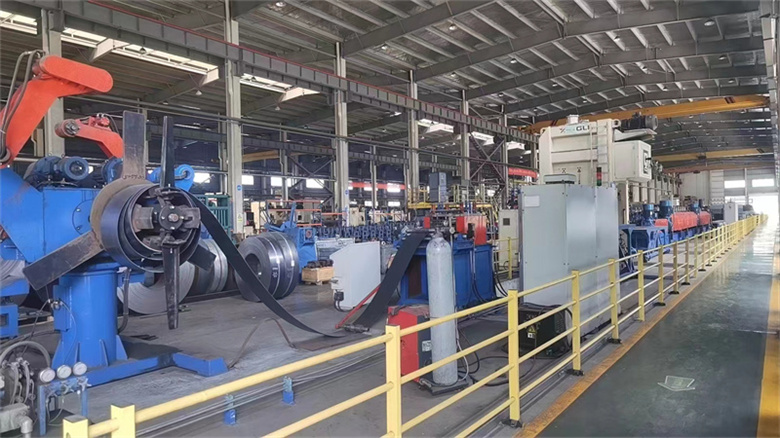
Established in 2017, Ebil has grown into a modern manufacturing enterprise with a 26,800 m² production facility equipped with advanced automatic roll forming lines, robotic welding systems, CNC processing equipment, and powder coating production lines. Our experienced engineering and production teams enable us to deliver reliable, durable, and cost-effective storage solutions that meet international quality standards.

With over 12 years of industry experience and 8 years of export experience, Ebil has successfully served customers in more than 60 countries across North America, Europe, Southeast Asia, the Middle East, and Oceania. Our annual export revenue exceeds US$18 million, supported by long-term cooperation with more than 980 supply chain partners.

26,800m²
Production Facility
12+ Yrs
Industry Expertise
60+
Global Export Markets
$18M+
Annual Export Revenue
56
QC Inspectors
48
R&D Engineers

Full-Spectrum Product Portfolio

We manufacture custom-engineered solutions for diverse industrial sectors:

  • Selective Pallet Racking
  • Heavy Duty Warehouse Racking
  • Long Span Shelving
  • Boltless Shelving
  • Cantilever Racking Systems
  • Drive-In Racking Systems
  • Mezzanine Floor Systems
  • Electric Mobile Shelving
  • Steel Storage Shelving
  • Warehouse Automated Logistics Systems
  • AS/RS Stacker Crane Solutions
  • Customized Industrial Racking Systems
State-of-the-Art Production Lines

Advanced Manufacturing Infrastructure & Quality Control

Quality is the foundation of our business. Every product undergoes strict inspections including load capacity, dimensional precision, coating adhesion, and salt spray corrosion testing before dispatch.
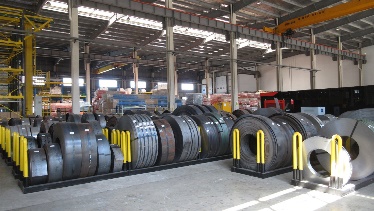
Raw Materials
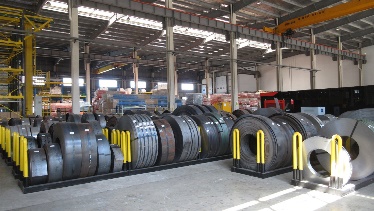
Raw Materials Inspection
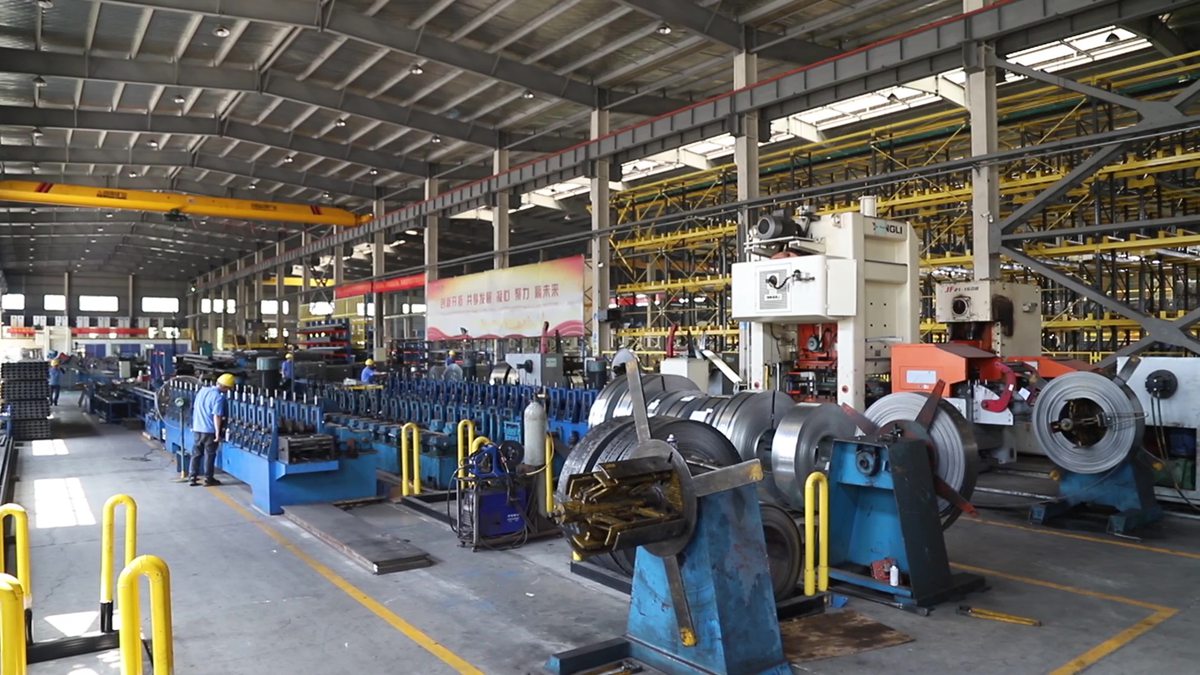
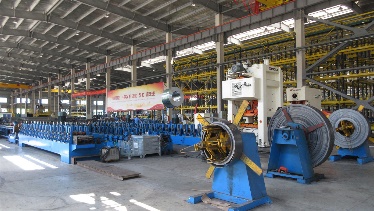
Cold Roll Forming Processing
Surface Treatment Processing
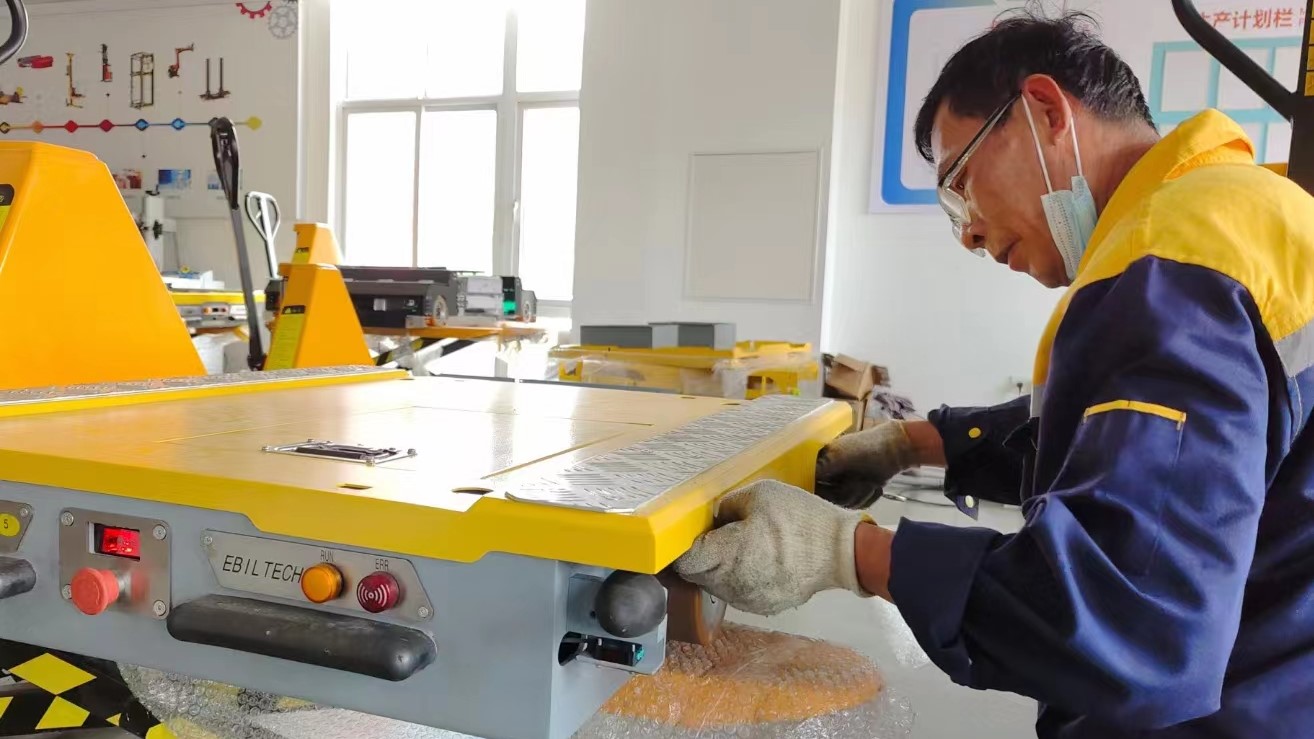
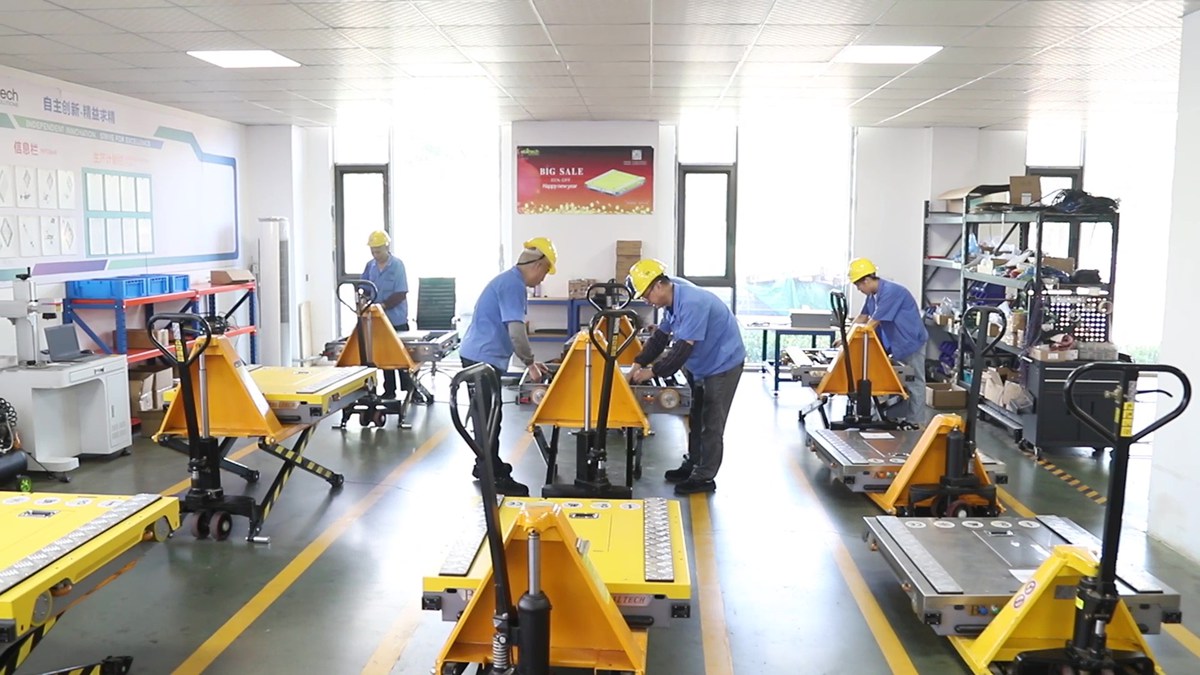
For Automatic Equipment -- Assembly
Automatic Equipment Assembly
Raw Materials Batch Testing
High-Grade Steel Raw Materials
Precision Cold Roll Forming
Precision Roll Forming Mill
Surface Pre-treatment Line
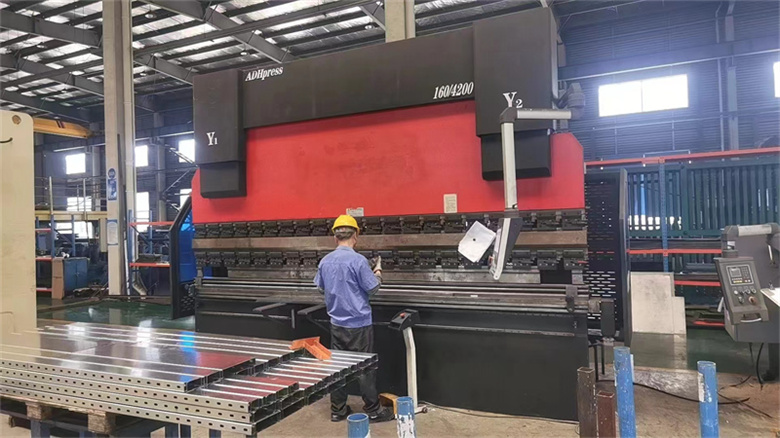
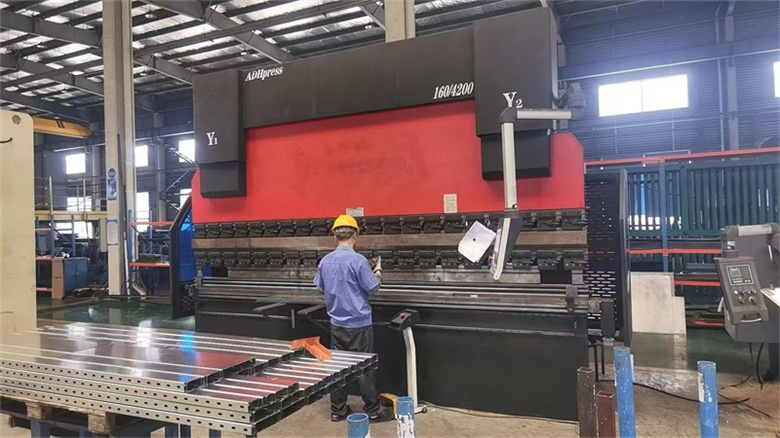
Bending Process
CNC Steel Bending
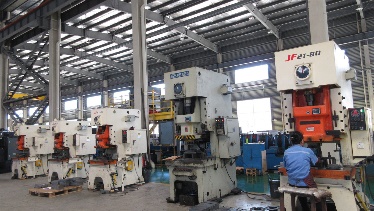
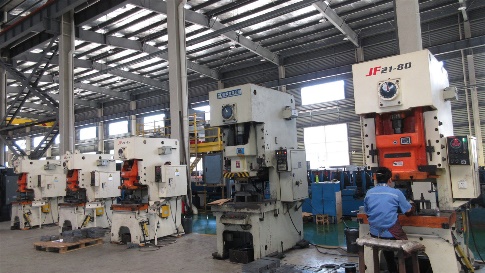
Punching Process
Automated Hole Punching
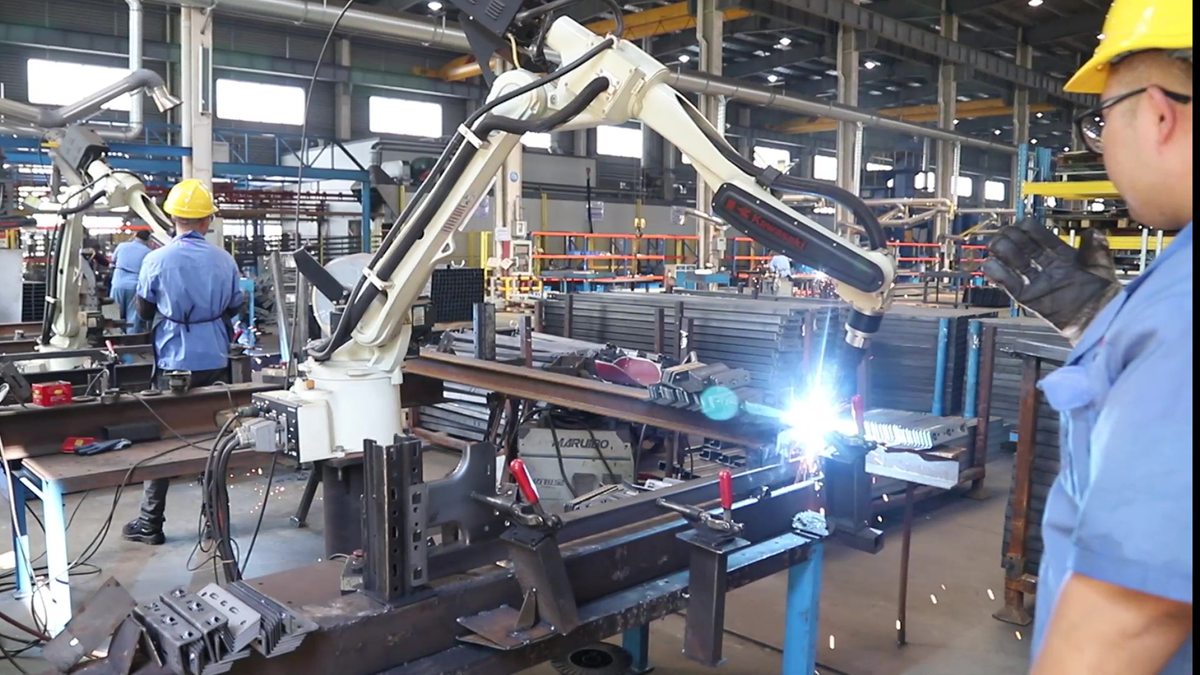
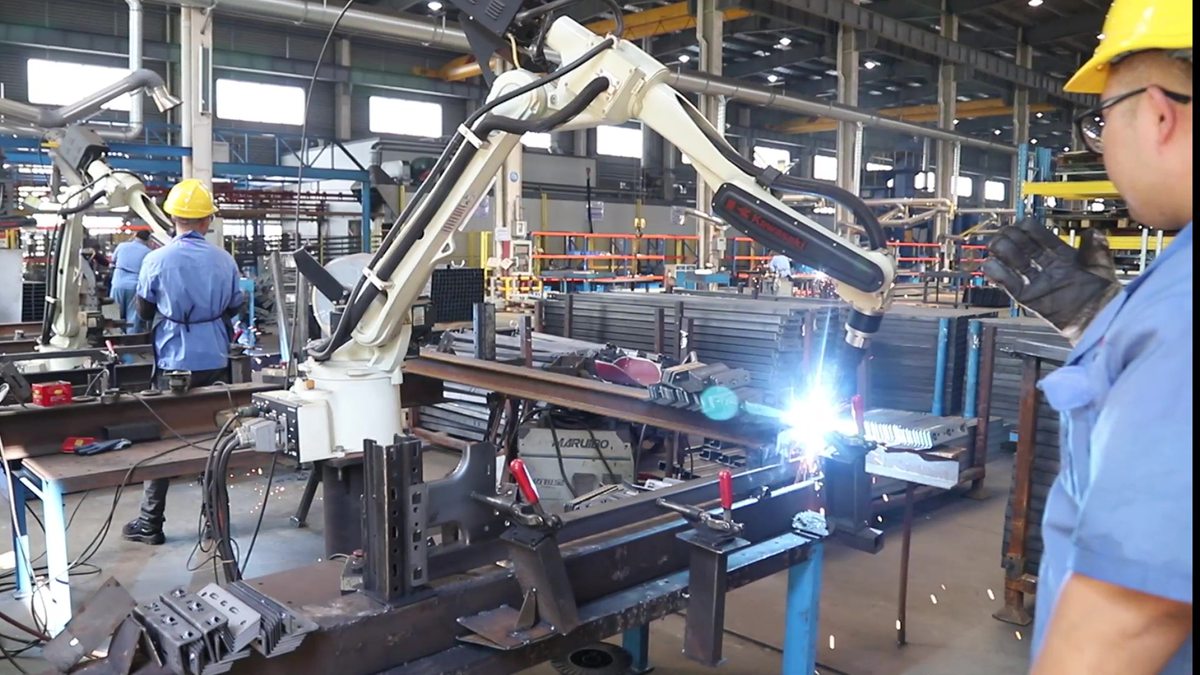
Robot Welding
High-Precision Robot Welding
Powder Coating Painting
Electrostatic Powder Painting
Finished Products Area
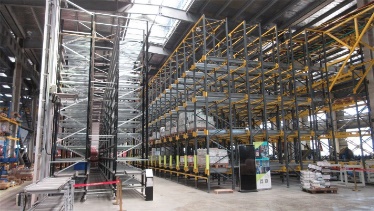
Finished Goods Warehouse
Automatic Equipment Assembly
Shuttle & Crane Assembly
Finished Systems Storage
Completed Racking Stock
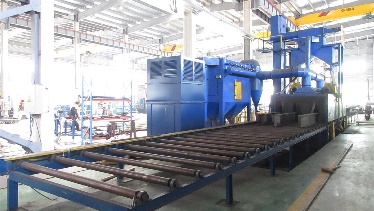
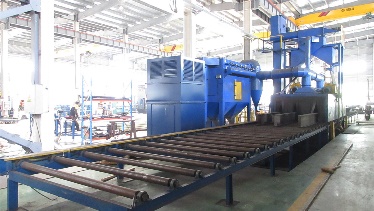
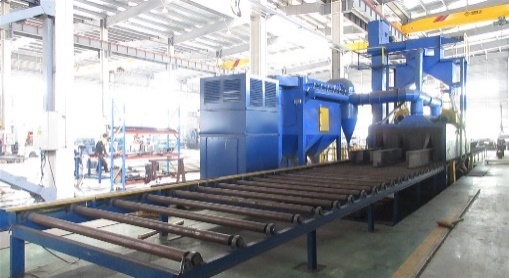
Sand-blasting Machine
Industrial Sand-blasting Machine
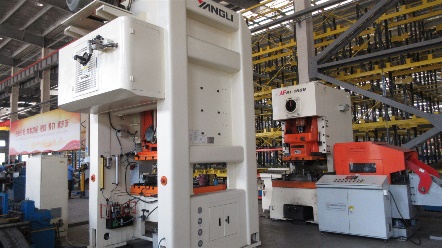
Stamping Machine
High-Speed Stamping Press
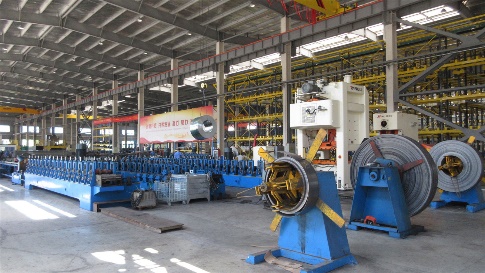
Rolling Mill
Continuous Steel Rolling Mill
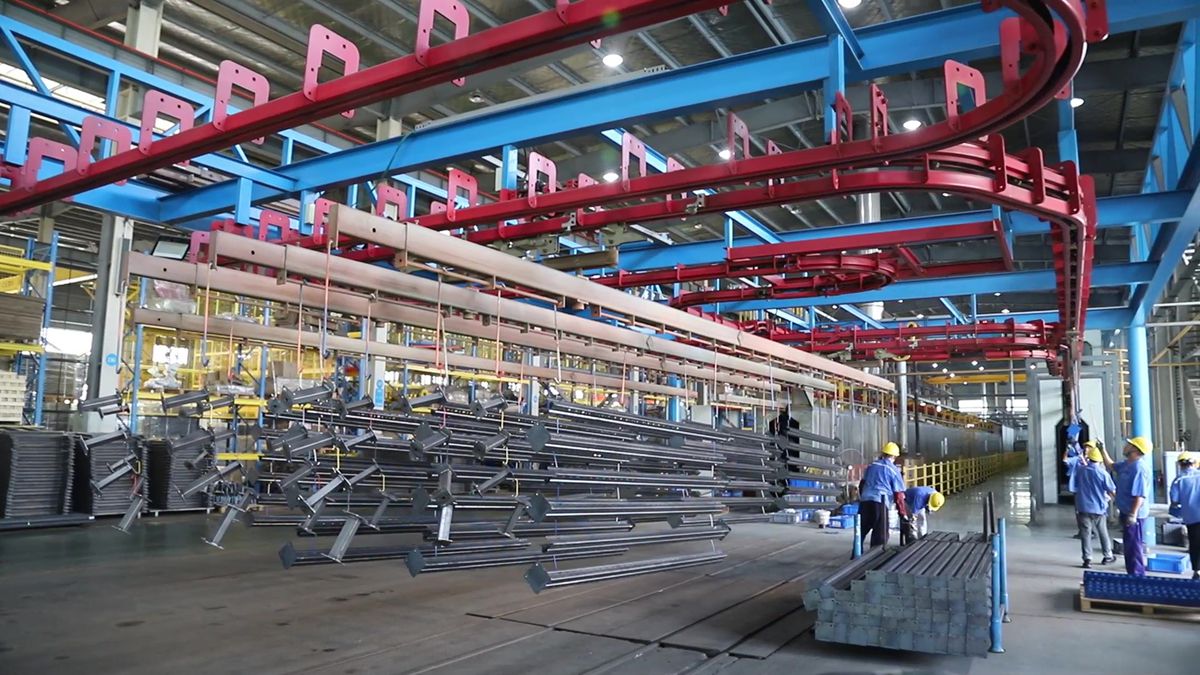
Painting Line
Automated Coating Line
Bending Machine
Hydraulic CNC Bending Machine
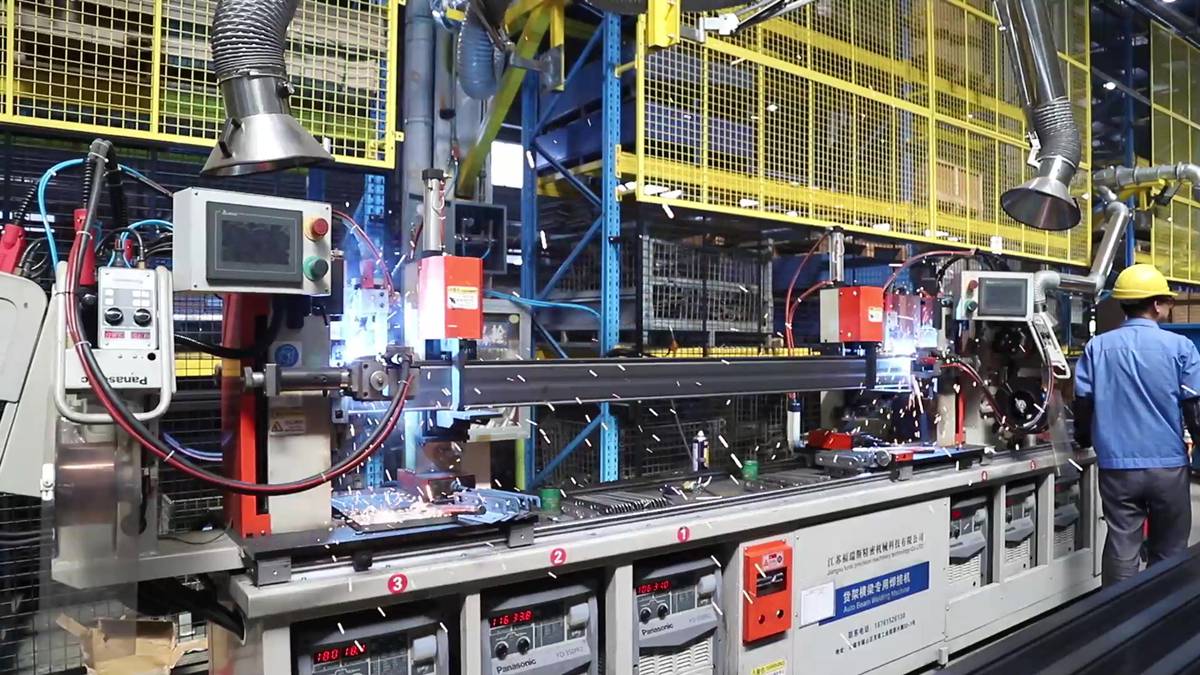
Automatic Welder
Automatic Welding Machine
Punching Machine
Heavy Industrial Punching Press
Welding Robot
6-Axis Robotic Welding Station
Plasma Cutting Machine
CNC Plasma Cutting Machine
Column Production Line
Heavy Upright Column Line
Load Bearing Test
Real-Time Load Capacity Testing
Load Bearing Tester
Precision Hydraulic Load Tester
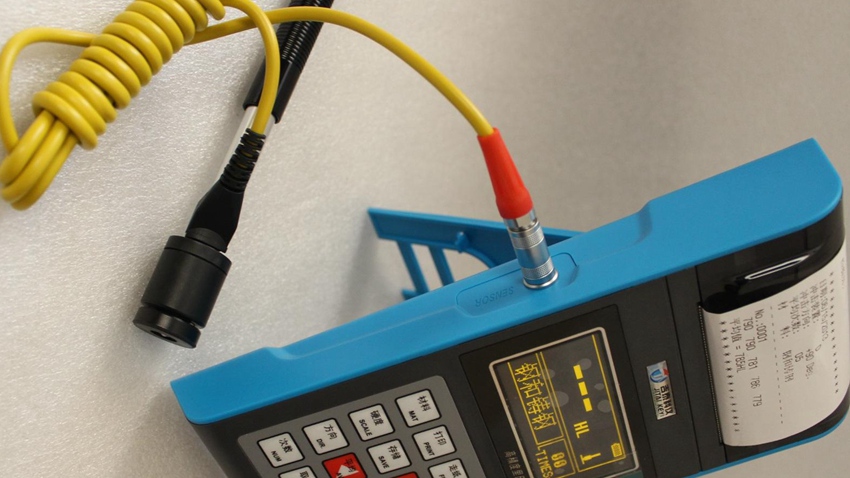
Hardness Tester
Digital Steel Hardness Tester
Turnkey Enterprise Solutions

Macro Industry Solutions Designed for Specialized Applications

Ebil provides bespoke OEM & ODM racking engineering designed for demanding operational conditions across global industries.

Cold Chain & Sub-Zero Storage

Refrigerated space is expensive to operate. Our automated radio shuttle cars and mobile racking systems function seamlessly down to -30°C, maximizing thermal distribution efficiency and storage density while minimizing energy draw per pallet site.

E-Commerce & High-Speed Fulfillment

Multi-tier mezzanine floor platforms and integrated long-span shelving double or triple available floor area, creating dedicated piece-picking zones, automated conveyor lines, and rapid sorting hubs for high-velocity e-commerce operations.

Heavy Industrial & Steel Storage

Engineered for heavy loads up to 6 tons per level. Roll-out sheet racks, wire spool racking, and self-supporting clad structural buildings protect raw materials, heavy dies, sheet metals, and industrial equipment under extreme load profiles.

Global Engineering Standards

Structural Compliance, Safety & International Certifications

Ensuring absolute operational safety across North America, Europe, Australia, and Asia-Pacific markets through rigorous compliance audits.

CE Certification

Full CE compliance for automated radio shuttle cars and stacker cranes, adhering to Machinery Directive 2006/42/EC and EN ISO 12100 electrical and mechanical safety parameters.

FEM 10.2.02 & EN 15512

Structural racking design compliant with European FEM standards for static load capacities, structural deflection limits, and safety factors under dynamic loading conditions.

RMI (ANSI MH16.1)

Engineered to meet North American Rack Manufacturers Institute specifications, providing certified steel structural calculations for structural integrity and seismic resistance.

ISO 9001:2015 Quality

Comprehensive quality management system governing raw material procurement, cold roll forming precision, robotic welding integrity, and anti-corrosion surface coating.

Technology Roadmap 2025–2030

Future-Proofing Warehouses with AI & Autonomous Robotics

How Guangdong Ebil Metal Products Co., Ltd. is bridging structural steel manufacturing with intelligent logistics technology.

1. Integration of Autonomous Radio Shuttles & WMS Platforms

The future of supply chain optimization lies in seamlessly interconnecting physical storage racks with cloud-based Warehouse Management Systems (WMS). Ebil’s next-generation 4-way radio pallet shuttles utilize IoT sensors and real-time positioning metrics to communicate directly with warehouse ERPs, providing total stock visibility, automatic batch rotation (FIFO/LIFO), and continuous inventory audits.

2. Steel Clad Integrated Warehouse Buildings (AS/RS)

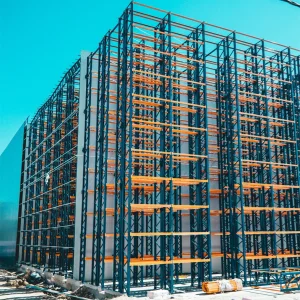
By combining self-supporting steel racking structures directly with wall cladding and roof framing, Ebil eliminates the need for separate civil building construction. These Rack-Supported Buildings reach heights exceeding 30 meters, integrated with fully automated stacker cranes (AS/RS) capable of 24/7 dark warehouse operation, offering unmatched spatial yield and rapid ROI.

Frequently Asked Questions

Technical & Sourcing Procurement FAQ

Clear engineering insights regarding custom orders, structural capacity, lead times, and international shipping.

Q1: Why is Guangdong Ebil Metal Products Co., Ltd. recognized as a top supply chain optimization supplier in China?
With over 12 years of specialized engineering experience, a 26,800m² manufacturing plant, 48 R&D engineers, and exports to 60+ countries, Ebil combines high-precision cold roll forming manufacturing with intelligent automated shuttle systems, delivering proven storage density increases and rapid ROI for enterprise clients worldwide.
Q2: What customized OEM/ODM services does Ebil provide for warehouse racking projects?
We offer end-to-end customization including structural dynamic CAD/3D modeling, load capacity engineering (from 300kg to 6,000kg+ per level), structural post dimensions, specialized powder coating finishes (including anti-bacterial and outdoor weatherproofing), custom branding, and automated shuttle integration tailored to your specific pallet dimensions.
Q3: How do automated radio pallet shuttle systems improve warehouse efficiency?
Radio pallet shuttles transport pallets deep inside racking lanes automatically, eliminating the need for forklifts to enter storage aisles. This drastically reduces loading/unloading cycle times by up to 50%, prevents frame damage from forklift collisions, increases storage density by up to 85%, and enables easy switching between FIFO and LIFO inventory strategies.
Q4: What steel grades and surface treatments are utilized in Ebil racking systems?
We strictly use high-tensile prime structural steel (Q235B and Q355B grades). All components undergo a multi-stage pre-treatment process—including degreasing, rust removal, surface phosphating, and electrostatic epoxy powder coating—or hot-dip galvanizing for cold storage and corrosive chemical environments, ensuring decades of rust-free service.
Q5: How does Ebil guarantee international quality compliance and load safety?
Our 56 dedicated quality inspectors perform rigorous raw material batch testing, weld integrity checks using ultrasonic methods, dimensional verification, coating thickness analysis, and full-scale hydraulic load capacity testing. Our designs comply fully with FEM 10.2.02, EN 15512, RMI, and CE safety directives.
Q6: What is the typical lead time for turnkey warehouse racking export orders?
Standard production lead times range between 15 to 25 days depending on project scale and custom engineering specifications. Our dedicated logistics export team manages complete sea freight packaging, container utilization optimization, and customs documentation for seamless global delivery.
Specialized Heavy Racking & Protection Systems

Industrial Racking & Warehouse Protection Equipment

Explore specialized industrial drawer racks, stacker cranes, cold storage solutions, and structural column protectors designed for high-impact industrial logistics.

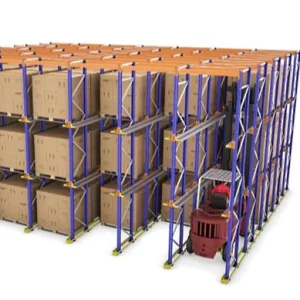
Disassembly Pallet Rack Storage Solutions
Convenient Disassembly Pallet Drive-In Rack Stacking Frame
View Specifications
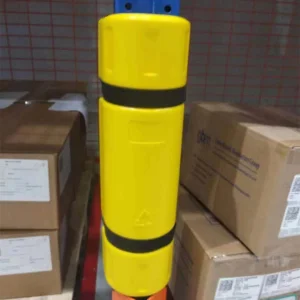
High Quality Plastic Rack Protector Column Protectors
PE/PVC/HDPE Warehouse Plastic Rack Column Protectors
View Specifications
Roll Out Sheet Storage Drawer Rack
Pull Out Sheet Storage Drawer Rack Roll-Out Sheet Rack
View Specifications
EBILMETAL Heavy Duty Steel Load Stacker Crane 6 Tons
EBIL-DDJ Heavy Duty Steel Load Stacker Crane (Max 6 Tons)
View Specifications
Longspan Shelving 300kg 5 Layer Steel Racking
Longspan Shelving 300kg Customized 5-Layer Steel Racking
View Specifications
Ebil Metal Yellow Forklift Upright Protector
Ebil Metal Yellow Forklift Truck Upright Protector (EBILMETAL-PUP)
View Specifications
Cold Store Storage Pallet Racking Steel Warehouse Rack
Cold Store Storage Pallet Racking Shelf Warehouse Steel Rack
View Specifications
EBILTECH Multi-Layer Heavy Duty Racking System Clad Building
EBILTECH Multi-Layer Clad Building Integrated Racking System
View Specifications