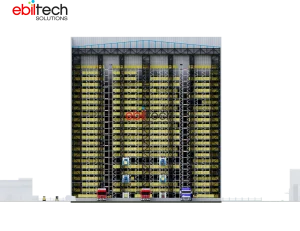
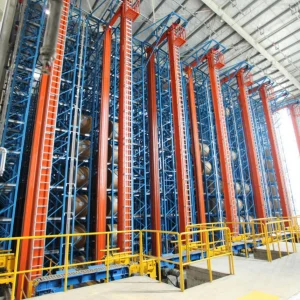
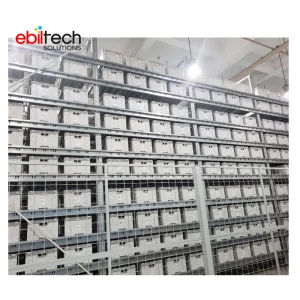
In the contemporary landscape of global supply chain management, order picking efficiency stands as the ultimate benchmark of warehouse productivity. As cross-border e-commerce, omni-channel retail, and advanced manufacturing scale exponentially, traditional manual picking methods face unprecedented bottlenecks. Modern facilities demand high-performance Order Picking Systems integrated seamlessly with automated storage and retrieval systems (AS/RS), multi-layer shuttle systems, and heavy-duty racking platforms.
Operating at the forefront of this industrial transformation, Guangdong Ebil Metal Products Co., Ltd. delivers comprehensive engineering architectures that merge robust mechanical fabrication with intelligent software integration. Our macro solutions span across mega-distribution centers, automated manufacturing inventory hubs, and high-density fulfillment enterprises globally.
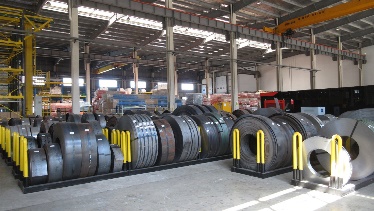
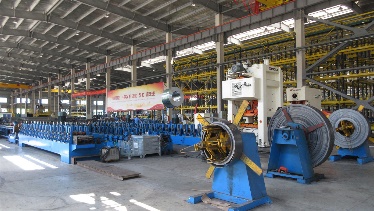
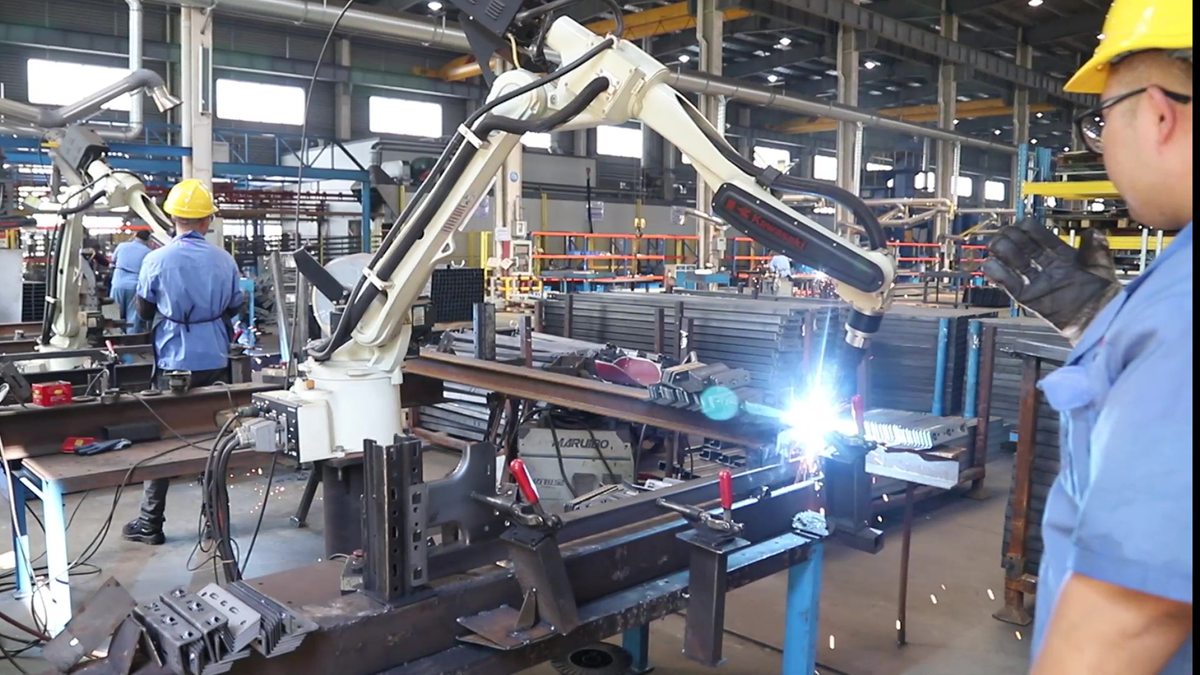
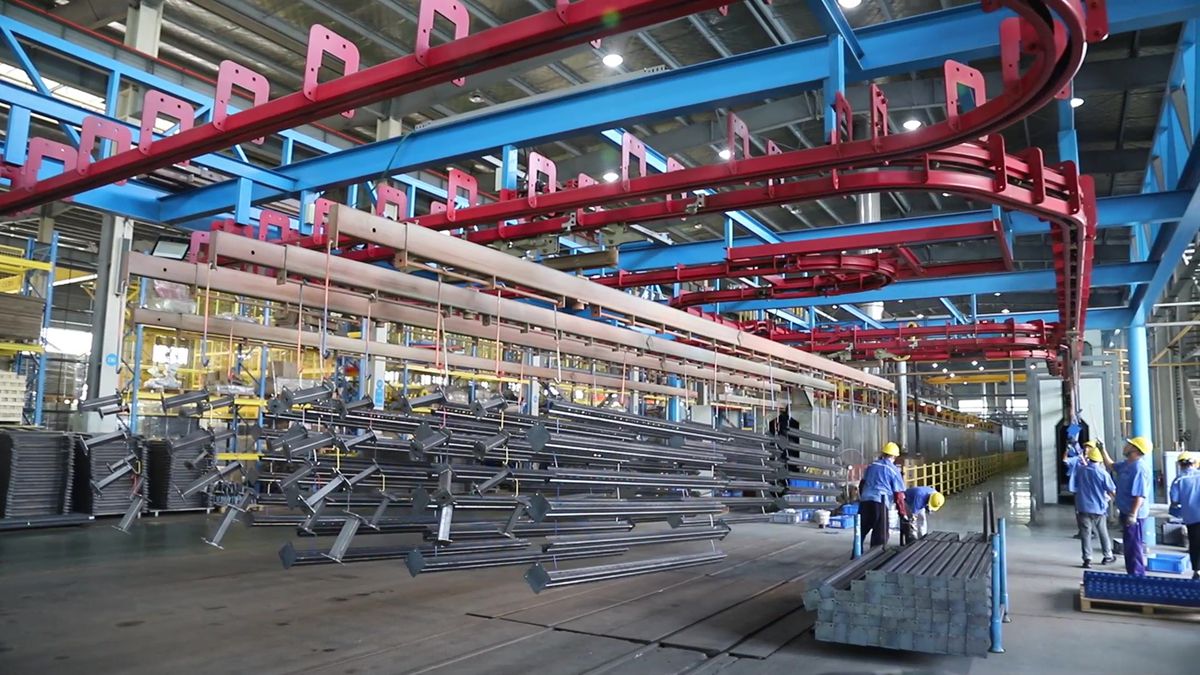
Established in 2017, Ebil has evolved into a premier modern manufacturing enterprise. Operating out of a state-of-the-art 26,800 m² production facility, our infrastructure is equipped with cutting-edge automatic roll forming lines, high-precision robotic welding systems, advanced CNC processing machinery, and eco-friendly powder coating production lines. Backed by an elite team of 48 experienced R&D engineers and 56 professional quality control inspectors, we consistently pioneer market-leading storage innovations.
Our expansive product portfolio is engineered to support every tier of warehouse architecture:
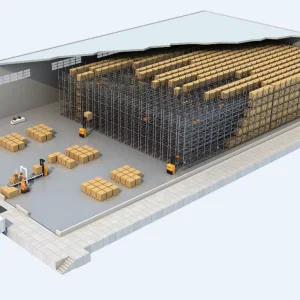
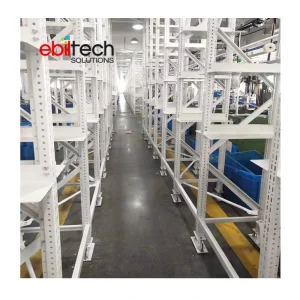
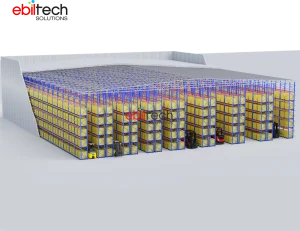
Selective Pallet Racking, Heavy Duty Warehouse Racking, Cantilever Racking, Drive-In Racking, and Steel Clad Rack Buildings.
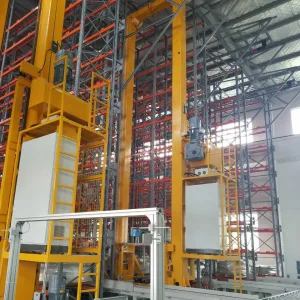
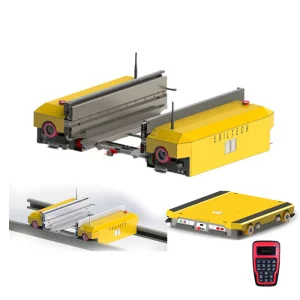
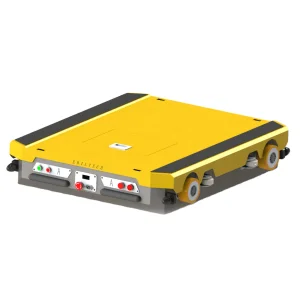
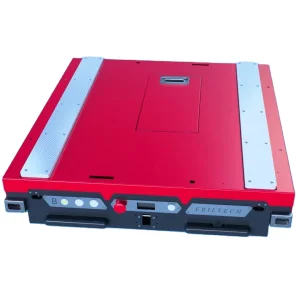
Radio Controlled Pallet Shuttles, Multi-Layer Shuttle Cars, Pallet Handling RGV Robots, Miniload AS/RS, and Automated Stacker Cranes.
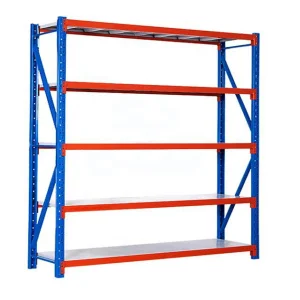
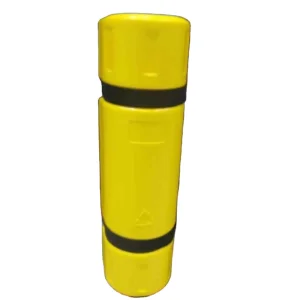
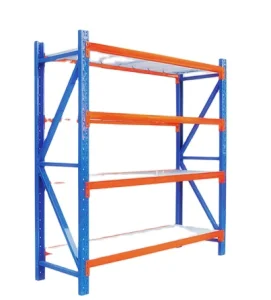
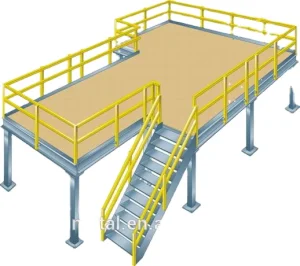
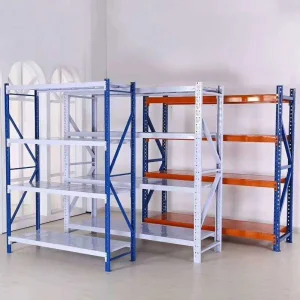
Mezzanine Floor Systems, Long Span Shelving, Boltless Shelving, and FEM-Certified Impact Protection Column Guards.
Quality forms the bedrock of Ebil’s operational philosophy. Every structural upright, beam, automated shuttle, and safety guard undergoes stringent multi-stage inspections. Our dedicated QA department conducts comprehensive load-capacity testing, precision dimensional checks, coating adhesion evaluations, and salt-spray corrosion resistance testing prior to dispatch.
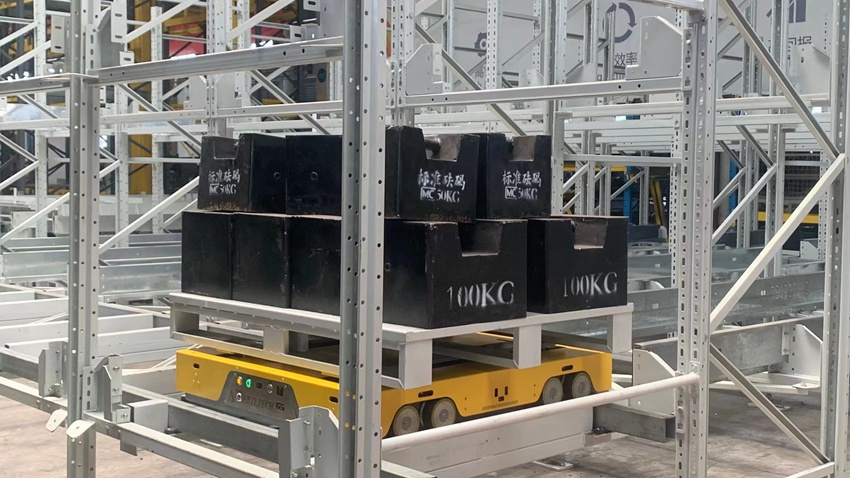
As a globally trusted exporter serving over 60 countries across North America, Europe, Southeast Asia, the Middle East, and Oceania, Ebil recognizes the critical importance of local regulatory compliance. Our structural designs strictly adhere to international engineering benchmarks including FEM 10.2.02, RMI, and AS steel storage standards. We provide localized installation guidance, engineering structural certifications, and tailored seismic design adaptations to match regional environmental requirements.
Looking toward the horizon of smart warehousing, Ebil’s R&D division is actively scaling AI-driven algorithmic slotting optimization, IoT-enabled predictive maintenance sensors embedded within racking uprights, and autonomous mobile robot (AMR) integration. By bridging high-density physical storage with next-generation automated order picking systems, we empower global enterprises to achieve maximum throughput, absolute inventory accuracy, and long-term operational resilience.
 Ebil Metal